Thursday, February 18, 2016

Brew A Partial Mash Beer

#homebrew Brew Boss Electric Homebrew Equipment EBIAB www.brew-boss.com #thebeernation


What Is A Partial Mash


Essentially in partial #mashing you are getting a portion of the fermentable sugars for the wort from a mix of base and specialty grains. It is anything but difficult and requires only a little more time and attention to detail compared to steeping grains. The only extra piece of equipment which maybe required is a good thermometer. You may also consider adding a bigger brew kettle to hold the entire volume of wort, a strong nylon bag to hold the grains, a device to quickly chill your hot wort to pitching temperature, and an aquarium pump and aeration stone to add oxygen to the wort.


Mashing (Partially)


Mashing is a simple process, but one that is often made to seem overly complex in some homebrewing texts. The essence of mashing is simply soaking crushed grains in water. As the grains soak, the water dissolves the starch in the grains. Enzymes from the grain attack the starch and chop it up into its building blocks, sugars. Once the starch is fully converted, the sugars are rinsed from the spent grains.

As far as starch-conversion goes, a partial mash works exactly like a full mash. However, since less grain is used in a partial mash, handling the soaking and rinsing of the grains is simpler and requires no special equipment beyond a mesh grain bag and a measuring cup. Performing a partial mash is very similar to steeping specialty grains. Gaining some experience with partial mashing often encourages brewers to go on to try making an all-grain beer.

Why Partial Mash?


So why perform a partial mash? That's a little harder to answer but lies in the type of grains a recipe may require when it was originally designed as an all-grain brew. If an all-grain recipe calls for a modest to high percentage of unmalted grains (examples: flaked grains or torrified grains) or non-steeping specialty grains (example: biscuit malt, aromatic malt, honey malt, etc…), or uses a base grain that does not have a malt extract equivalent (example: rauch malt, Vienna malt, mild malt, etc...), then it is a good candidate for making a partial mash.

As already mentioned, in mashing the starch in the center of malted grains is broken down into its constituent sugars. By adding in some base grains with the unmalted or specialty grains, we get the enzymatic power to convert the starch into sugar, which the unmalted or specialty malt would be incapable of doing on its own. Here at BYO we always try to simplify all-grain recipes that have been submitted to an extract format for home brewers. Some all-grain recipes easily can be converted to extract only, some require the use of steeping grains like crystal or roasted malts, while some require performing a partial mash and some just really can't be converted at all.

Performing a Partial Mash


In a partial mash, the goas is to steep the grains in a volume of water sufficient to cover them completely, but not leave a lot of excess volume. For our partial mash stout we'll steep 1.5 pounds (0.68 kg) of pale malt, plus the equivalent amount of specialty grains, in 2 gallons (7.6 L) of water. This is a thinner mash than most full mashes, but that won't adversely affect our beer.

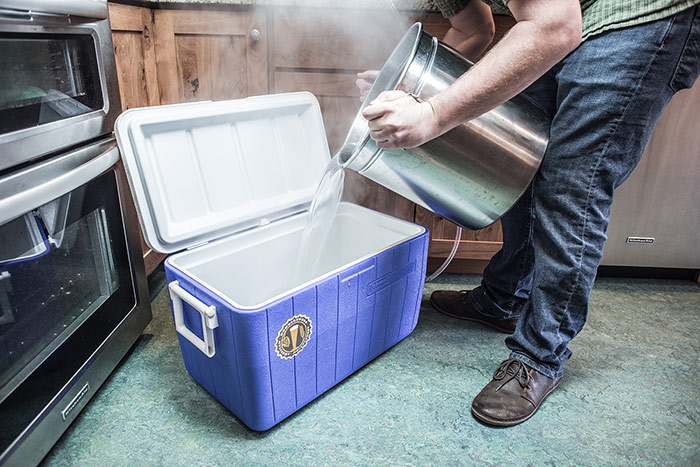
To begin the partial mash, gather the crushed grains and place them in the nylon bag. Although we will be holding the temperature of the mash at 150 °F (66 °C), we need to heat the water to 160 °F (71 °C) to start. This is because the temperature of the mash will drop once the grains, which are at room temperature, are added to the liquid. Once the grain bag has been submerged for a couple minutes take the temperature of the water in the pot and you can add heat or cold water to adjust the temperature of the mash if needed. Try to hold the temperature as close to 150 °F (66 °C) as possible for 1 hour. If the pot you are mashing in is oven safe, you may consider placing the mash in your oven at "keep warm" or about 150 °F (66 °C).

As you heat a pot, it takes time for the heat to travel through the metal and equilibrate. Thus, if you heat the mash continuously until the thermometer reads 150 °F (66 °C), then turn off the burner, the temperature will keep rising as heat from the pot is transferred to its contents. To avoid this, heat the mash in short bursts, stir while heating, and wait a couple of minutes before checking the temperature again. It's not going to hurt the beer if it takes you a little while to adjust the temperature, so be patient.

Rinsing the Grains (Sparging)


After an hour, take a large kitchen strainer and lift the bag out of the water. Let the liquid drain into your pot. If possible, balance the strainer over the pot. If you can't do this, have a friend hold it. Make sure that the grains are exposed before you begin rinsing them. Take a measuring cup and ladle hot water over the grains. The water will run through the grains rinsing out the sugar still trapped in the grain. Keep doing this for 5 minutes or so. The idea here is to rinse (sparge) as much of the sugars from the grains as possible. A good rule of thumb is to run an equal amount of rinsing water as you added initially to the mash, so 2 gallons (7.6 L) for our stout. 

Full-Wort Boil (Optional)


The remainder of the suggestions in this article are for those folks stepping up to full-wort boils as well as a solid recipe for 1st time (or 20th time) partial mash brewers. While not a necessity, we do highly recommend full-wort boils, not just for partial mash brewers, but for all homebrewers for the reasons listed below. For more reading and recipes on partial mash brewing, we recommend checking out these two great articles by Chris Colby, first this as well as this one.

Reasons to Perform a Full-Wort Boil

In your large brewpot — it should hold at least 8 gallons (30 L) of liquid — combine the wort from the partial mash with water to make 5.5 gallons (21 L). Bring this to a boil, then add the malt extract. Although our target is 5 gallons (19 L) of wort, we need more wort initially because some liquid will evaporate during the one-hour boil. The amount that evaporates is dependent on the amount of heat applied to the kettle. If you're boiling on the kitchen stove, the evaporation may be minimal; if you're using a propane burner, it may be considerable.

Boiling 5 gallons (19 L) of wort is a large task for most home stoves. A gas stove can probably bring this volume of wort to a rolling boil. An electric stove may have problems developing more than a sustained simmer. Also, the amount of time it takes for the wort to come to a boil may be quite long. You may wish to begin heating the additional water while you are performing the partial mash. If your kitchen stove is having trouble boiling this volume, close the lid partially.

Two benefits of boiling the entire wort are increased hop utilization and less wort darkening compared to boiling a concentrated wort. When brewing a beer using a full-wort boil, you need to add fewer hops to get the same level of hop bitterness. This is because more hop bitterness is extracted in more dilute worts. With a full-wort boil, you can also brew beers that are much lighter in color than beers brewed with from a concentrated wort. In thicker worts, the sugars carmelize much easier, darkening the wort. This difference in color won't be very visible in any darker colored beer though.

Another change that a full-wort boil will bring is the inability to pour the wort directly into the fermenter. (Pouring boiling wort into a glass carboy, for example, could crack the glass.) With no cold water to dilute the wort and bring down the temperature, you will need to cool the wort first. Then, given the large volume, it's more convenient to simply siphon the wort to the fermenter.

This drawback, however, has a hidden benefit. Since siphoning the wort to a fermenter leaves behind material on the bottom of the kettle, you don't need to keep your hops in a bag or tea ball. The hop debris will settle to the bottom of the kettle during cooling. The clear wort can then be siphoned off the hop material and hot break, the proteins, lipids and other compounds that coagulate in the boil.

Cooling your Wort

There are several ways to cool wort. One way is to place the kettle in a sink or bathtub full of cold water and ice. The drawback of this method is that you need to lift a large volume of near-boiling hot liquid. Needless to say, this can be a bit dangerous. You can avoid the potential hazard of spilling 5 gallons (19 L) of hot wort by chilling it on the stovetop with a submersible wort chiller.

A submersible wort chiller is a spiral of copper or stainless steel tubing. This tubing is submerged in the wort and cold water is run through it. Heat from the wort transfers to the cold water and is carried out. The speed of cooling and the eventual temperature the wort reaches depends on the temperature of the cooling water.

You can speed chilling by gently whirlpooling the wort. If the submersible wort chiller is left undisturbed, the wort next to the copper coils will quickly cool. However, the wort farther away from the coils will cool much more slowly. The wort will move somewhat in that cold wort will sink and warmer wort will rise. But, starting a whirlpool will greatly enhance the amount of hot wort passing by the copper coils and greatly enhance your cooling rate.

If you move the submersible wort chiller in a circular motion, you will start the wort moving. As the wort moves by the cool chiller, it cools. Hot wort is prone to hot-side aeration, so try not to agitate it unduly. Induce a slow, steady swirling motion by moving the wort chiller in a circle. Repeat this motion every five minutes.

The wort chiller is usually sterilized by submersing it in the wort for the final 15 minutes of the boil. During this time, there is no water flowing through it. In fact, it's best not to connect the tubing until after you have turned off the heat to the kettle. A logistical note: Connecting the tubing to your sink faucet will probably require an adapter, since most wort chillers are threaded to screw onto a garden hose connector.

Aerating the Wort

Performing a full-wort boil necessitates one other change in your brewing procedure; you should aerate your wort once it is cool. When extract brewing, we simply add cold, aerated water to our concentrated wort to aerate it. Now we can't do that, because our wort is already at working strength. Adding water would dilute it.

One of the simplest ways to aerate cooled wort is by using an aeration stone attached to an aquarium pump. Most aeration "stones" used in brewing are actually made of stainless steel. Air is pumped into the stone, where it is forced out through hundreds of tiny holes. Air from the aquarium pump should be filtered, so you are not pumping airborne microorganisms into your wort. Most homebrew shops sell aeration kits that include the stone and a HEPA filter. Since the aeration stone and the tubing leading to it will touch the wort, you must sanitize both before you aerate.

You can aerate your wort while it is siphoning into your fermenter. Just put the aeration stone in the fermenter and run the aquarium pump as you are siphoning. By the time your fermenter is filled, the wort should have enough oxygen. If you'd like, you can run the pump for another five or ten minutes. However, keep an eye on the wort so the bubbles from the aeration stone don't make the wort foam over.

Dry Irish Stout

OG = 1.048 FG = 1.014
IBU = 30 ABV = 4.6%

Ingredients
3.5 lbs. (1.6 kg) extra light dried malt extract
1.5 lbs. (0.68 kg) pale ale malt (Maris Otter is preferred)
1.5 lbs. (0.68 kg) flaked barley
1 lb. (0.45 kg) roasted barley
9 AAU Fuggles hops (60 min.)
(2 oz./57 g of 4.5% alpha acids)
Wyeast 1968 (Londong ESB Ale) or White Labs WLP002 (English Ale) or Safale S-04 yeast
3/4 cup corn sugar for priming

Step by Step
If you opt to use one of the liquid strains, then 4 days before brew day make a 1-L yeast starter. Refrigerate yeast starter 1 day prior to brew day and decant the liquid just prior to pitching the yeast.

On brewing day, heat 2 gallons of water to 160° F (71 °C). Steep the crushed pale ale malt and flaked barley for 45 minutes. Hold temperature at 150 °F (66 °C). Add the crushed roasted barley to the nylon bag and hold for 5 more minutes. Place grain bag in a kitchen strainer and rinse grains with approximately 2 gallon (7.6 L) hot water. Top off to 6 gallons (23 L) of wort and heat. Stir in malt extract (preferably while heat is turned off momentarily to avoid scorching) then bring wort to boil. Add the bittering hops and boil for 60 minutes. Turn off the heat then cool wort with wort chiller (or cold tub of water). Siphon cooled wort to fermenter. Aerate wort with aquarium pump, stone and filter, then pitch yeast. Ferment for one week at 68 °F (20 °C). You can then rack the beer to a secondary if you prefer, but this is an optional step. Two weeks after brew day test specific gravity with hydrometer for 3 straight days. If the specific gravity remains constant, go ahead and bottle, adding the priming sugar to your bottling bucket. After bottling, condition for 2 weeks, preferably in a slightly warmer than normal room. Your beer should now be fully carbonated and ready for you to enjoy. Cheers!

https://byo.com/newbrew/partial-mash

Tuesday, February 16, 2016

Video: Swirl-Boss Homebrewing Whirlpool Device

#Swirl-Boss #Homebrewing #Whirlpool Device by #BrewBoss
Simple device attaches to your brew pump to whirlpool your wort prior to transferring to the fermenter. A specially milled "E" Nozzle directs jets along the kettle wall as well as inward at the optimum angle to produce the fastest rotational speed of the whirlpool. Clamps onto any brew kettle with stainless steel clamp. Adjust to a position just below the surface of the wort. Also aerates the wort for better yeast health.

Available at www.brew-boss.com.

http://www.brew-boss.com/category-s/125.htm


Sunday, February 14, 2016

Fill-Boss Automated #Bottle and #Growler filler for Beer and Wine

Video Introduction to the #Fill-Boss automated bottle and growler filler for beer and wine made by Brew Boss for #homebrewers. Uses counter-pressure bottle filler technique to minimize foaming when filling carbonated beverages.


BUY the Fill-Boss now at the Brew Boss website!

http://www.brew-boss.com/category-s/157.htm


https://www.youtube.com/watch?v=HbqD_TKQwtY


Friday, February 12, 2016

Enzymes in Beer: What’s Happening In the Mash

#beer www.brew-boss.com Electric Homebrew Equipment #BIAB
Enzymes in Beer

As #homebrewers, we’re usually never satisfied until we know how things work. We constantly ask why and how something is done until we understand the basic concept. When you start brewing #all-grain, you hit a certain temperature to hit a specific characteristic because you were told to do so. You start picking up on words like alpha-amylase, beta-amylase, mash out and protein rest, and now you’re more curious than ever about what’s going on in the mash.

Here we’ll discuss the #enzymes in beer, which convert the starch in malt into soluble sugars. By understanding and making enzymes work for you, an all-grain brewer can control a multitude of components in their beer. Here is a list of the attributes of a beer that can be controlled during the mashing process:

  • Aroma
  • Flavor
  • Body
  • Overall mouthfeel
  • Attenuation
  • Color
  • Alcohol content

What Are Enzymes In Beer?


Enzymes are proteins that are found practically everywhere—your saliva and digestive system, plant photosynthesis, and most importantly, your livers. They have an important role as a non-living biomolecule because they catalyze biochemical reactions. Each enzyme is made up of several thousand different amino acid chains which take on specific shapes suited for specific jobs. In other words, they make reactions occur quickly and at the temperatures of living organisms. They join molecules together, take large molecules apart and rearrange molecules into something different.

Each biochemical reactions is catalyzed by a very specific enzyme. The molecule the enzyme acts on is called a substrate, and the enzyme is usually named after the substrate (i.e. Beta-Glucanase acts on Beta-Glucans). Just know that the enzyme’s shape is fragile and can be damaged by a multitude of factors, thereby rendering the enzyme unable to act as a catalyst. This is called denaturing the enzyme, and once it’s been damaged, it’s very difficult to renature it.

The rate at which the chemical reaction occurs is affected by temperature, enzyme and substrate concentration and pH. Enzymes catalyze reactions more quickly as temperature increases in their specific range. But, they’re also denatured by heating above their specified range, and reach peak activity just before they are destroyed.


Mashing Enzymes In Beer


All the enzymes you’ll need for conversion are present in the final malt. The malting process develops enzymes that reduce starches and proteins during malting and mashing, which helps create better clarity, head retention and body.

For homebrewers, we are concerned with the activity of two primary enzymes in beer: alpha- and beta-amylase.

Alpha-amylase breaks down large, complex, insoluble starch molecules into smaller, soluble molecules for the beta-amylase. It is stable in hot, watery mashes and will convert starch to soluble sugars in a temperature range from 145°F to 158°F.

Remember that the temperature range is important because as you reach higher temperatures, the denaturation process increases and enzymes are mostly gone within five minutes. Pouring grains into hotter “strike” water to account for temperature drops can cause problems, too. Exposure to hotter temperatures even for a few seconds can affect enzymatic activity, so make sure to get your temperature down as quickly as possible.

Beta-amylase is the other mash enzyme capable of breaking down starches and creating soluble sugars. After the alpha-amylase enzymes create smaller soluble molecules, the beta-amylase enzymes create most of the fermentable sugars by breaking down starch to create maltose, glucose and maltose. These enzymes help create lighter bodies and more alcohol and are most active from 131°F-149°F. As the temperature approaches 149°F, these enzymes are operating extremely fast, but are also being denatured quickly. In short, if the mash is held at a temperature within the beta-amylase range, then a greater proportion of soluble sugars will be maltose and thereby be more fermentable.

Temperature Rests in the Mash


Mash temperatures play a very critical role in determining the body, fermentability and developing the aroma and flavor profile of your beer. Depending on the style of beer brewed and the type of malt and/or adjuncts used, a different mash temperature or a combination of temperatures and schedule may be best for the brewing beer.


Influencing Factors on Denaturing Enzymes in Beer


Alpha and beta-amylase act together to degrade starches to produce a range of soluble sugars in the wort. Below a certain temperature (149°F), alpha-amylase activity is low and so the large starch molecules remain insoluble because the enzyme is unable to break them up. Same goes for above a certain temperature (150° F), beta-amylase activity is hindered, limiting the amount of fermentable sugars for the wort.

These temperature ranges are small, and leaves little room for a brewer to operate and influence the types of sugars that end up in the wort. A lower temperature results in a wort that is more fermentable but may yield slightly less, while a higher temperature will yield less fermentability but increased extract efficiency. Here are some important influencing factors on denaturing enzymes in beer.
  • Enzyme and substrate concentration
  • Temperature
  • pH

Enzyme & Substrate Concentration


Enzyme and substrate concentration is how concentrated your mash is, and mostly dependent on mash thickness. Although not a critical factor, mash thickness is still important to consider when you start mashing. A thick mash is anywhere between 1-1.25 quarts water/pound of grain.

A thick mash gives a quicker starch conversion and is more beneficial for protein breakdown because it offers better protection for your enzymes (i.e. beta-amylase). It’s more suited for step mashes because enzymes are not denatured as fast by temperature increases. A thin mash is anywhere around 2 quarts water/pound of grain, which dilutes the concentration of enzymes and thereby gives them less protection, a slower conversion, but provides a more fermentable mash because the enzymes are not inhibited by a higher concentration of sugars.

Temperature


Each enzyme has an optimum temperature, the temperature at which the enzyme is most active. Once the temperature goes below or above the temperature range, you affect the productivity of that enzyme. Think about a cold morning. You’re lethargic and slow, but as it warms up you start to move faster and your energy improves. However, if it gets too hot, you start to slow down again. This is essentially how enzymes work. More specifically, the active site on the enzyme changes and the substrate that pairs with the enzyme will no longer fit and becomes inactive.

pH


Mash pH is another factor that affects the activity of various enzymes. It should fall within a range of about 5.2 to 5.5 for the primary enzyme activity. If you mash using distilled water, you’ll end up with a pH in between 5.8 and 6.0. Adding calcium ions to the water will cause the mash pH to drop down into the 5.5 to 5.6 range, with additional calcium ions dropping it further. You’ll want to use a pH strip to calibrate your water pH level as you mash.

Key Take Aways
  • Although enzymes are fragile, they are reusable and generally affected by temperature and pH.
  • Enzymes have an optimum temperature and pH that they are most active.
  • Enzymes have a significant affect on finished beer and are also present in yeast cells.
  • Understand the primary mash enzymes (alpha and beta-amylase) and their optimal temperature and pH levels to achieve best results.
  • It’s important to understand the factors that denature enzymes.
  • Know what you want to accomplish before deciding your mash technique.

Sources: “Making Enzymes Work For You” by Randy Scorby, BJCP Continuing Education Director and Grand Master II Judge, 2015 National Homebrewers Conference Seminar

Thursday, February 11, 2016

Brew-Boss Product Release: Stainless Steel Ripple Heating Element


#Brew-Boss introduces it's newest product! We have developed a stainless steel #ripple heating element that has an integrated L6-30P plug and a 1.5 inch Triclamp ferrule. The element is ULWD, 5500 watts, 240 volts. We also have 120 volt 1500 watt foldback elements as well with teh same L6-30P and Triclamp ferrule. This element eliminates the issues when trying to build your own electric brewing system related to how to connect the wires to the element and properly enclose the connections and properly ground the element. This element solves all those problems. All you need to do is add an L6-30R receptacle on your controller and install a 1.5" triclamp ferrule on your kettle. Of course the Brew-Boss kettles and controllers are natural mates to this heater!


Order yours today!
http://www.brew-boss.com/ULWD-L6-30P-Stainless-Steel-Ripple-Heater-Element-p/htr-5500-ripple-l6-30p.htm


www.brew-boss.com

#electricbrewing #homebrew #brewboss

Wednesday, February 10, 2016

Understanding Water for Homebrewing


Discussions about water can get complicated fast, especially if you aren’t familiar with hydrology. But there are a few basics that specifically apply to the homebrewer, which can set the foundation for further exploration into the realm of brewing water.

Let’s take a look at the four key aspects of water that relate to homebrewing and how they affect the beer making (and drinking) process.

pH


pH is the measurement of acidity in water. The amount of concentrated hydrogen ions determines where a sample of water will fall on the 0-14 pH scale. A neutral reading (seven) indicates there is an even balance of hydrogen and hydroxide ions. Anything below seven treads into acidic territory, and above seven towards the base side of the scale.

The affects of pH begin in the mash and follow through to the last sip of a pint. pH influences everything from enzymatic activity and fermentability to color and taste of beer, making it a crucial aspect of water. However, it is a common misconception that water must be a certain pH prior to brewing. While this is somewhat true, the real concern is achieving a certain pH in the mash and ultimately in the kettle. After all, mash pH directly affects kettle pH, and kettle pH ultimately impacts how the character of beer will be perceived on the palate.

Ideally, mash pH should be in the range of 5.1-5.8 (5.2-5.5 being optimal). When lautering, it is key to ensure that the pH of the runoff is not above 5.8, since this is when astringent, lip-puckering tannins can make their way into the kettle. Many brewers who have issues with runoff pH being too high will use phosphoric acid to acidify the sparge water. The final beer should be in the 4.2-4.4 pH range to achieve optimal taste and stability. Brews above 4.5 will likely exhibit heavier, harsher character with a lacking freshness. Below 4.0 can start to create a thin drinking experience and even add an unintentional tartness.

Hardness


Chances are you’ve heard of “hard water” before, especially if you live in an area that has hard tap water. Hardness was originally developed to indicate how difficult it is to get soap to lather in the water sample, which is not all that useful when it comes to homebrewing beer. However, hardness can also be used as an indicator of the amount of calcium and magnesium ions in water.

Hardness is categorized as either temporary or permanent. Temporary hardness is a signifier as to how much calcium carbonate is present, which can be reduced by boiling the water and allowing the calcium carbonate to precipitate out. Permanent hardness on the other hand is based on the amount of sulfates and chlorides present.

While hard water might not be pleasant to drink, the calcium present is key to brewing, so it’s not typically a priority to reduce the hardness of brewing water.


Alkalinity & Residual Alkalinity


Alkalinity is a measurement of how much a water sample will resist a change in pH, otherwise known as water’s buffering capacity. Hydroxide, carbonate and bicarbonate ions primarily contribute to alkalinity, which undergo reactions with acidic substances that increase water’s pH value. On water reports, alkalinity is often times recorded as the amount of bicarbonate or calcium carbonate.

Because much of the United States water sources have medium to high alkalinity, it can cause the mash pH to increase, which can cause mash efficiency issues and carry over into the final beer as an overall dullness and other unfavorable characteristics.

The alkalinity remaining in solution after phosphates present in malt react with the calcium and magnesium water, which precipitates out insoluble salts lowering the pH, is termed residual alkalinity. In the end, it is largely the residual alkalinity and the acidity of the malts being mashed that will determine the mash of the pH and affect the outcome of the final beer.


“Flavor” Ions


Sometimes called stylistic ions, flavor ions are the most important when it comes to affecting beer character. Flavor ions include sodium, chloride and sulfate, while calcium and magnesium mainly affect hardness and carbonates and bicarbonates affect alkalinity. Together, all three groups affect pH and mash chemistry, which impact the flavor of the final beer.

Calcium is arguably the most important ion for brewing. It affects enzymatic activity in the mash, protein coagulation during the boil and benefits yeast health. Clarity, flavor and stability of the final beer all rely on calcium. Ideally, the mash should have 50-200 ppm or calcium.

Magnesium also affects mash pH, but to a lesser extent than calcium. It mainly enhances flavors and sourness when present at lower levels. 10-30 ppm of magnesium will help this flavor accentuation and act as a yeast nutrient, but as concentrations exceed 50 ppm, an unpleasant sour-bitterness and astringency can become apparent.

Sodium also helps round out flavors, particularly accentuating malt sweetness, at an ideal concentration of 70-150 ppm. In higher concentrations (>200 ppm), sodium can add harsh salty-sour notes and potentially become toxic to the yeast.

Chloride accentuates a fuller body and sweetness in beer, particularly in malt-forward styles. In appropriate quantities it will also improve stability and clarity, but in excess it can cause a harsh drinking experience.

Sulfate, on the other hand, accentuates a dry crispness and hop bitterness in beer, particularly in hop-forward styles. If concentrations exceed appropriate amounts, a harsh, sulfury quality can be instilled and the hop bitterness can come across as harsh.

Bicarbonate is the primary source of alkalinity in beer. Its role affects the pH, more specifically the ability to alter the pH, of wort and ultimately the final beer.

Sources: Brewing Better Beer: Master Lessons for Advanced Homebrewers by Gordon Strong; The Oxford Companion to Beer by Garrett Oliver et al; Water: A Comprehensive Guide for Brewers by John Palmer and Colin Kaminski; “Water: The Role of Residual Alkalinity” by John Palmer (July/August 2008 Zymurgy)

Monday, February 8, 2016

How to Build a Hop Oast

#beer #hops #brewboss www.brew-boss.com Electric Homebrew EquipmentDIY-hop-oast-featured


Hop Oast

One of the more substantial costs for homebrewers from batch to batch is hops, especially if you want to homebrew lots of American styles—IPA and Double IPA (and variants) in particular. Finding a way to keep costs down on hops isn’t as simple as re-pitching yeast or filling spray bottles full of Star-San. Though some brewers have supposedly dry hopped a beer and then put those hops into the kettle for bittering another brew, I’d recommend not doing this as you don’t know what kind of bittering you will get, and what do you do with the hops between brews to ensure they don’t spoil?

We’d like to suggest another, more effective ways to save money on hops. I like to buy hops in bulk, but this can still be costly. So I decided to grow them. Check out past posts on and learn how to grow hops and harvest and prepare hops for brewing. This post explains how to build a Hop Oast to dry hops.


Construction

  • Parts Needed: (around $30)
  • 7 pieces 2x4x8′ kiln-dried fir
  • 48″ x 7′ aluminum screen material roll
  • 3″ wood screws (56)
  • Staple gun
  • Box knife
  • Cordless drill

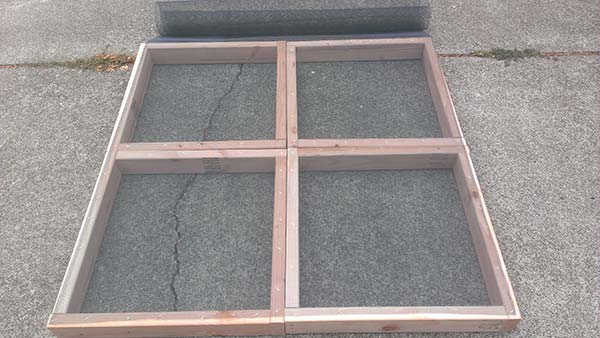
Begin by cutting each board into 4 – 23″ pieces (keep the scraps). I just had the guy at Lowes do this for me. Take each of the pieces and begin screwing them together using two screws to each joint. Align each joint so that they are flush on top and bottom, and that the end of one board is flush with the side of the next at a 90° angle. Don’t go overboard to insure a perfect angle as it will self align when you make the last connection. Once you have all four corners drilled together, set the tray aside. Repeat this until all seven trays are built.


After you have all seven trays built, set one aside. Place the others together two wide, and three tall on a flat surface. I did this on my driveway. Once they are flush and straight, roll the screen out over the top of them. The 48″ width should be a perfect fit across two trays, and the 7′ should easily cover the three trays up. Once you have the screen spread over, use the staple gun to attach it to the corners, then work your way around all of the trays along every side rail and every corner until each tray is fully attached to the screen.


Now take your box knife and insert the blade between two trays through the screen and cut along the separation until all the trays are cut apart. You will have a little hangover from the edges, feel free to clean them up with your box knife, I just left mine for now (more important to get the hops dry when you build this after the bines have been cut down). It would be good to glue along the inside edge and allow it to dry to seal the trays from allowing hops to get stuck between the screen and box frame, and it will make cleaning easier after you are done with them.

After they are separated, take the small scrap pieces and use them to raise a box fan off of the ground a few inches. This will give you air flow to go up and through your hops. You will want to pick a place where there will be some heat, air flow for the humidity to escape, and that is not in direct sunlight. I used my garage and put a space heater next to it to blow under the fan since we had a cold front hit when I got the hops picked. I didn’t let it run unattended. I only did this on the weekend while I was home as I did not trust the space heater to run while I wasn’t home or while asleep.

Place the screenless tray on top of the box fan as a diamond for use as a base. If your box fan is large enough, you can stack it on top at the same angle as the box fan edges, but for mine, it worked perfect to turn it slightly so that it became a diamond to the square fan, creating an eight pointed star if outlined. This empty tray with no screen allows a little extra flow for the fan so it isn’t blowing directly against the screen and hop bed which may cause it to overheat.

Function

At this point, you should pick your hops into sacks and weigh them. It is always more fun to have a helper. Place a single variety into a single (screened) tray. Once your tray is full (about 1/3 up the side), set it on top of the base tray over the fan so that the tray edges align perfectly over each other. Continue to pick your hops, fill your trays and stack them up. Leave one of the trays empty to the side. I used a piece of masking tape to mark each tray to know which variety was in which tray. Next year, I may just add a plastic sleeve to the side and make up cards with the names of the varieties I grow to sort them that way (it will look much nicer).

Once your trays are filled with hops, place the last empty tray on top. This tray’s screen will keep things from falling into your hops, and keep the stray hop leaves in place to make clean up a little easier. At this point, turn on your fan to medium. Low will take longer, and high would be faster, but you don’t want to have it so high that you end up blowing any of the lupulin out of the hops.

Leave the hops to dry for a few days, gently fluffing them up every 12 hours or so to ensure even drying. I also swapped trays out so that the bottom trays became middle trays, top became bottom and middle became top. I continued this rotation whenever I fluffed them. They say that the hops should be about 20 percent the weight they were when you picked them. If you got one pound of hops, you should have around 3-3.5oz of dried hops. Another telling sign is that when you take a hop cone and bend it in half the strig in the middle should snap clean. If if bends and moves back then they are still too moist.